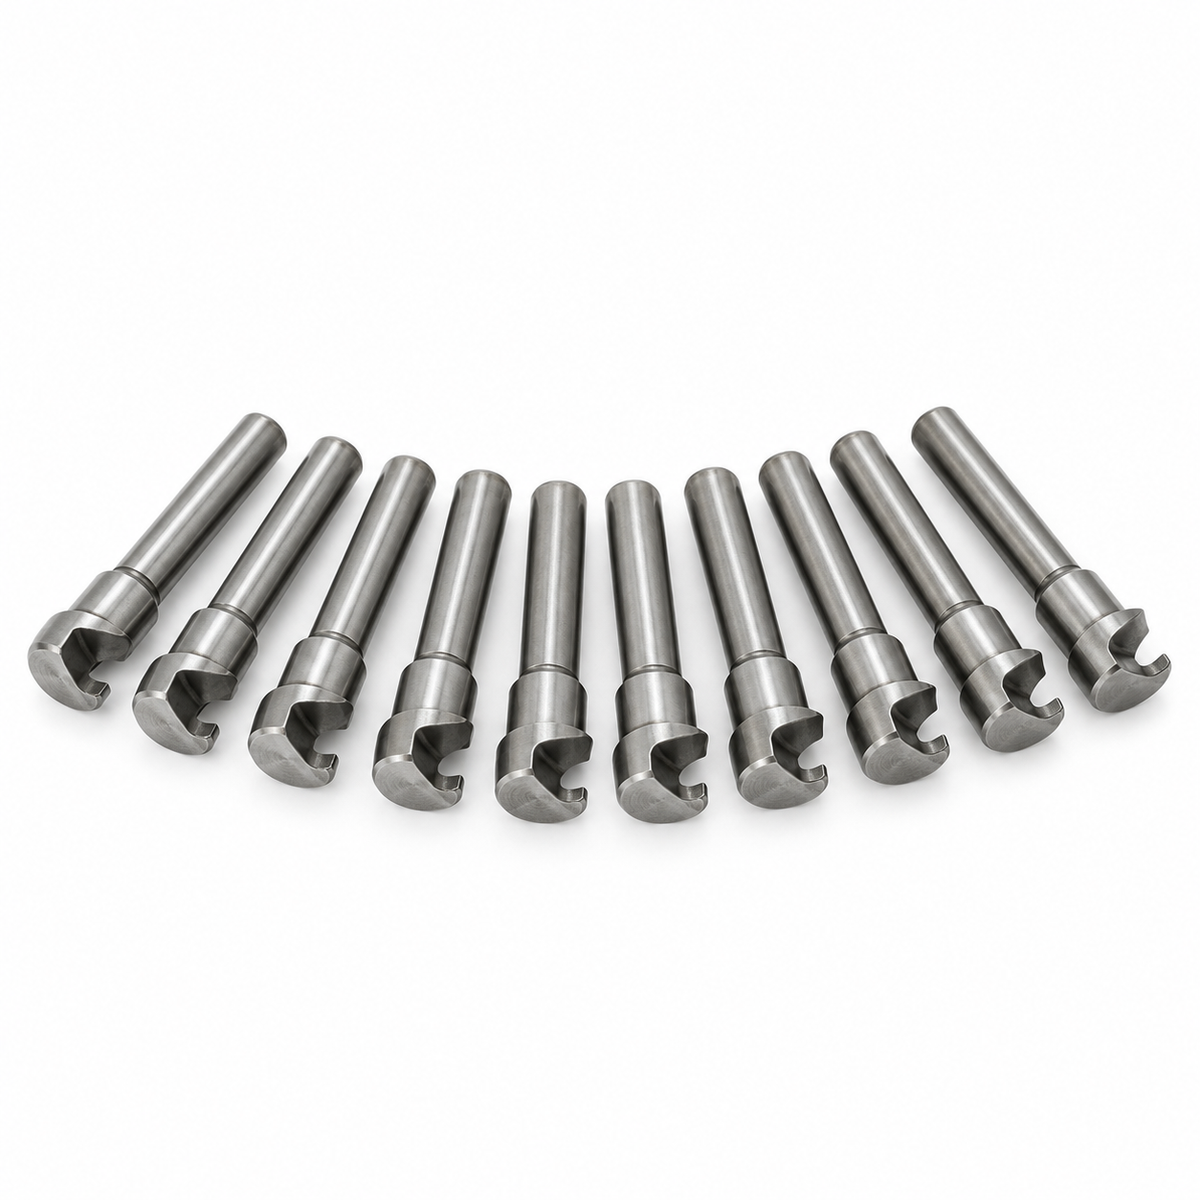


Hardened Runner Puller Pins, Z-Type — Pack of 10
Standard-part returns: request authorization within 14 days after delivery; item must be unused, uninstalled, undamaged and in original packaging. Review the full return policy.
Need a non-standard size? Request a Quote →Hardened runner puller pins (sprue pullers) for injection molds, sold in packs of 10. Sizes are given as diameter × overall length in millimetres.
What the puller actually does
The runner puller holds the cold runner and sprue on the moving half as the mold opens, so the sprue comes out of the fixed-half bushing rather than staying in it. It then releases the runner on the ejector stroke. That is two jobs with opposite requirements — grip on opening, release on ejection — which is why a puller that is slightly wrong causes trouble that looks like it is coming from somewhere else.
Too little grip and the sprue stays in the bushing: the mold opens, the runner hangs on the fixed half, and the next shot short-fills or the operator is picking sprues out with pliers. Too much grip and the runner will not let go of the puller on ejection, so it rides back into the closing mold. Most of the "the robot keeps missing the runner" complaints on a new tool are a puller geometry problem, not a robot problem.
Choosing the undercut form
These are supplied with a Z-type (angled undercut) head, the general-purpose form for cold-runner molds with a standard three-plate or two-plate layout. If your runner is deep, tapered, or the material is stiff and glass-filled, the alternatives worth knowing about are:
- Ball / spherical head — releases more readily, less positive grip. Suits soft and slippery materials that let go too easily from a Z.
- Reverse taper (conical) — pulls straight, releases straight, wears more evenly than a Z on abrasive filled resins.
- Mushroom head — strongest grip, hardest release. For deep runners on tools where the sprue is heavy.
If you are replacing a puller that was working, match the form you took out rather than what looks similar in a catalogue. If you are fixing a mold that never worked properly, tell us the resin and the runner cross-section and we will suggest a form.
Fitting notes
The pin has to be flush with, or very slightly below, the runner floor. Proud of the floor and it becomes a flow obstruction, packs differently on either side and can leave a witness on the part. Well below the floor and the undercut is not fully engaged in the plastic, so grip becomes intermittent — the puller works on nine shots and fails on the tenth, which is the hardest kind of fault to diagnose.
Also check that the puller bore is vented. A blind puller pocket traps gas at the end of the runner, and the resulting burn shows at exactly the point the tool builder least expects.
Specifications
| Head form | Z-type angled undercut |
| Condition | Hardened |
| Diameters | Ø4, Ø5, Ø6, Ø8 |
| Lengths | 30, 40, 50, 60, 70 mm (Ø8 from 40 mm) |
| Pack quantity | 10 pieces |
| Origin | Danyang, Jiangsu, China |
Intermediate lengths in 2 mm steps exist across this whole range and are not all listed here. If you need one between the sizes shown, ask — it is a stocked size, not a special.
A note on price and diameter
You may notice Ø4 is not the cheapest option. Small-diameter ground pins carry more grinding time per piece than the next size up, so cost does not simply follow steel mass. We price from actual supplier cost rather than smoothing it into a tidy ladder, so the numbers occasionally look counter-intuitive. They are the real figures.
Need something else?
Other head forms, non-standard undercut angles, longer pins and material-specific hardness are all made to order. Request a quote on the custom runner puller page with your geometry, or send a sketch of the runner section and we will propose the form.
Upload a sketch or dimensions and request a written quotation →
Shipping
International freight is calculated on packed chargeable weight. See Shipping & Delivery for destinations and transit times. Import duties and taxes are the buyer's responsibility — please read the duties section on that page before ordering.
- Material grade
- Confirm before ordering
- Hardness / load grade
- Confirm before ordering
- Surface treatment
- Confirm before ordering
- Key tolerance
- Confirm controlling dimensions before ordering
- Metric specification
- Diameter × overall length (mm)
- Package quantity
- 10 pieces per pack
- Single-piece weight
- To be confirmed
- Package weight
- To be confirmed
- Country of origin
- Danyang, Jiangsu, China
- Processing time
- Varies by specification; confirm before ordering when timing is critical
- International freight
- Quoted from packed chargeable weight; carrier transit time is estimated separately
- Typical application
- Cold-runner and sprue retention during mold opening
- How to select
- Match pin diameter, overall length and Z-type undercut geometry.
- Check before ordering
- Diameter, length, head/undercut form and runner release clearance
- Non-standard dimensions
- Submit an RFQ with a drawing, photo or measured dimensions